.jpeg)
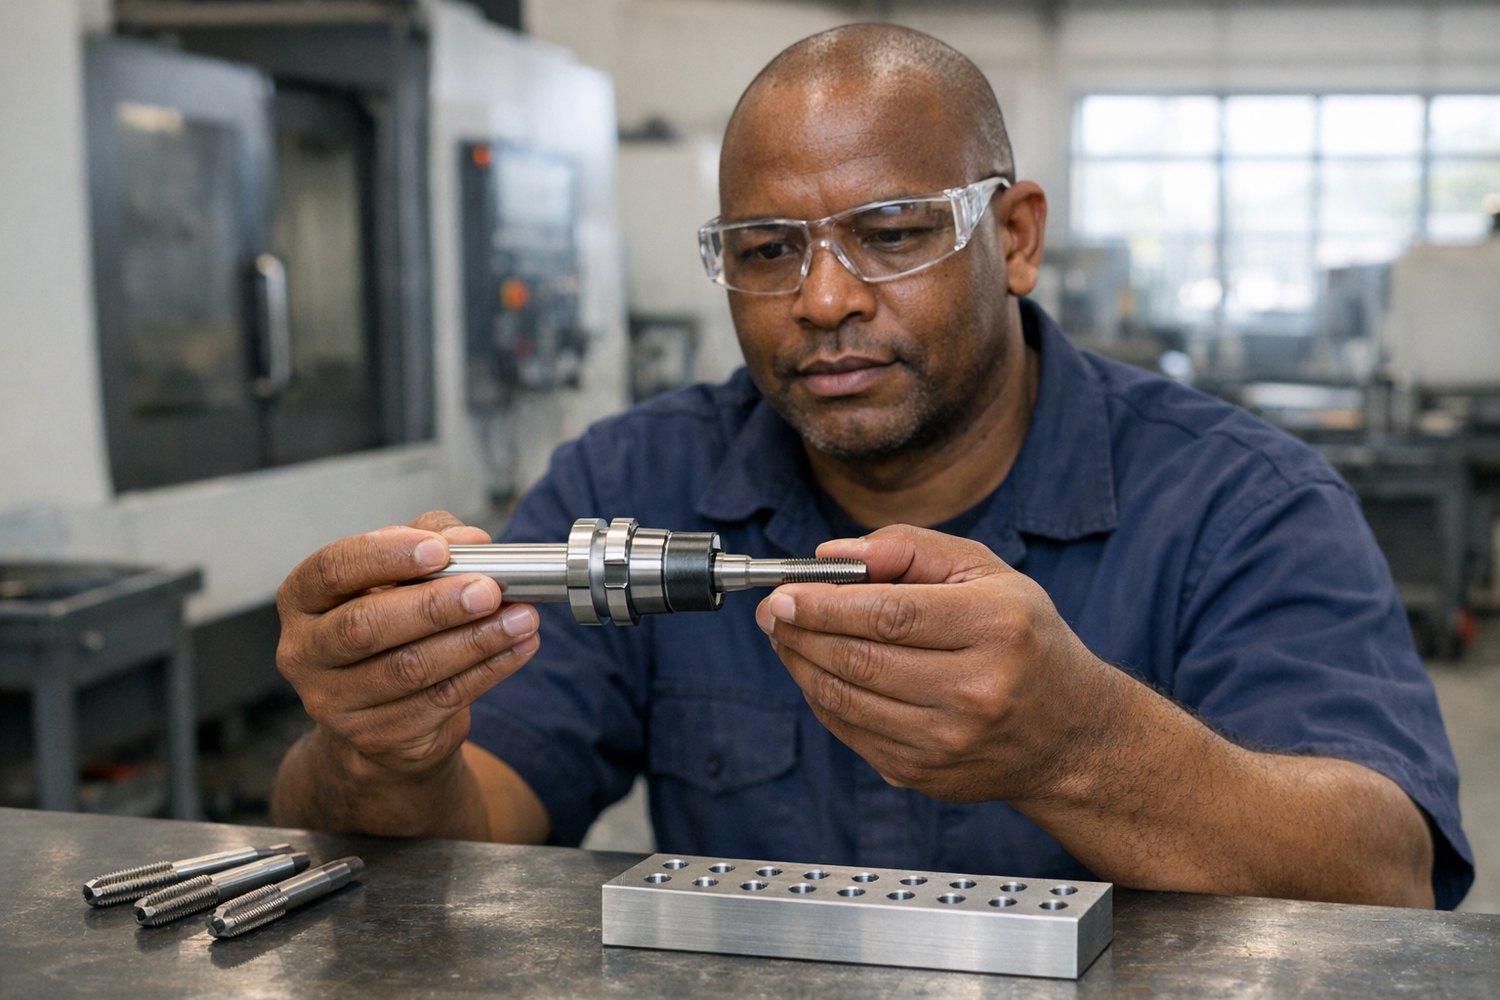
A machinist checks the machine tap clamped in a tapping holder at the bench before the next job, at a machine shop in Gqeberha.
The Struandale supplier now stocks synchro tapping holders, tension-compression chucks, torque-limiting adapters and ER tapping collets for broken taps.
GQEBERHA, SOUTH AFRICA, October 27, 2026 /EINPresswire.com/ -- Tooling, the Struandale, Gqeberha supplier of toolholders, workholding and machining equipment, has added CNC tapping holders and torque-limiting adapters to its catalogue. The range is meant for job shops, subcontract machinists and production plants in Markman, Coega, Kariega and Despatch, and for machine shops further afield that buy from the Struandale base.
A tap has a harder job than most cutters in the magazine. It has to stop at the bottom of the hole, reverse and come back out along exactly the same helix. If the spindle and the Z axis are even slightly out of step at that moment, the tap gets pushed or pulled along its length. In aluminium that might only show up as a thread that gauges loose. In steel, stainless or cast iron it usually means torn threads and chipped teeth, and sooner or later a broken tap stuck in a part that already has an hour of machining in it.
Most modern machining centres have rigid tapping, and that solves a lot of it but not all. Servo lag, worn ballscrews on older machines and the sudden reversal in blind holes still leave a small mismatch. Tooling's synchro tapping holders have a small axial float, usually a fraction of a millimetre, that takes up that error instead of passing it into the tap. For older CNCs, drilling machines and lathe work where feed and spindle aren't locked together, the company supplies tension-compression chucks with several millimetres of float in and out.
The range also covers quick-change adapters with a clutch that slips when torque goes past the set value, which matters most on small taps in blind holes, and ER tapping collets with a square drive for shops already running ER collet chucks. Holders come in BT30, BT40, SK40 to DIN 69871 and HSK-A63, plus straight-shank versions for lathes with driven tools, with through-coolant options for coolant-fed taps.
"When a customer phones about broken taps, the tap is usually the last thing we look at," said Tooling's toolholding specialist. "We ask about the machine, whether rigid tapping is actually switched on, what the drill size was and whether the holes are blind. A lot of the time the fix is a holder that can float a little, and a clutch set for the tap size instead of cranked up because one slipped."
Before quoting, the team asks for the machine make and spindle taper, tap sizes and shank standard, material, hole depth, coolant type and any tool-length limits in the magazine. Forming taps need more torque than cutting taps of the same size, so they change the clutch setting. Tooling also checks tapping holders, collets and adapters for runout and wear as part of its existing runout check service, and presets tapping assemblies with the rest of a customer's tools.
Tooling's advice also covers restarts after power cuts. When the machine stops with a tap still in the hole, the team says to reverse it out slowly at low speed, or back it out by hand where the controller allows, and inspect it before the next cycle. A tap that breaks on the next part was often damaged at the restart.
About Tooling
Tooling has supplied precision tooling, workholding, CNC machines, 3D printing and scanning equipment to South African machine shops since 2008. From its base in Struandale, Gqeberha, it also offers tool regrinding, inspection, runout checks, presetting and collection and delivery for workshops in Markman, Coega, Kariega, Despatch and the Gqeberha CBD, with nationwide delivery. It is part of the same South African trade network as equipment supplier am.co.za. Tooling is operated by Astros Marketing (Pty) Ltd, 2 Makro Place, Sunnyrock 1401.
Poppy
Tooling
+27 60 600 6000
Legal Disclaimer:
EIN Presswire provides this news content "as is" without warranty of any kind. We do not accept any responsibility or liability for the accuracy, content, images, videos, licenses, completeness, legality, or reliability of the information contained in this article. If you have any complaints or copyright issues related to this article, kindly contact the author above.
